
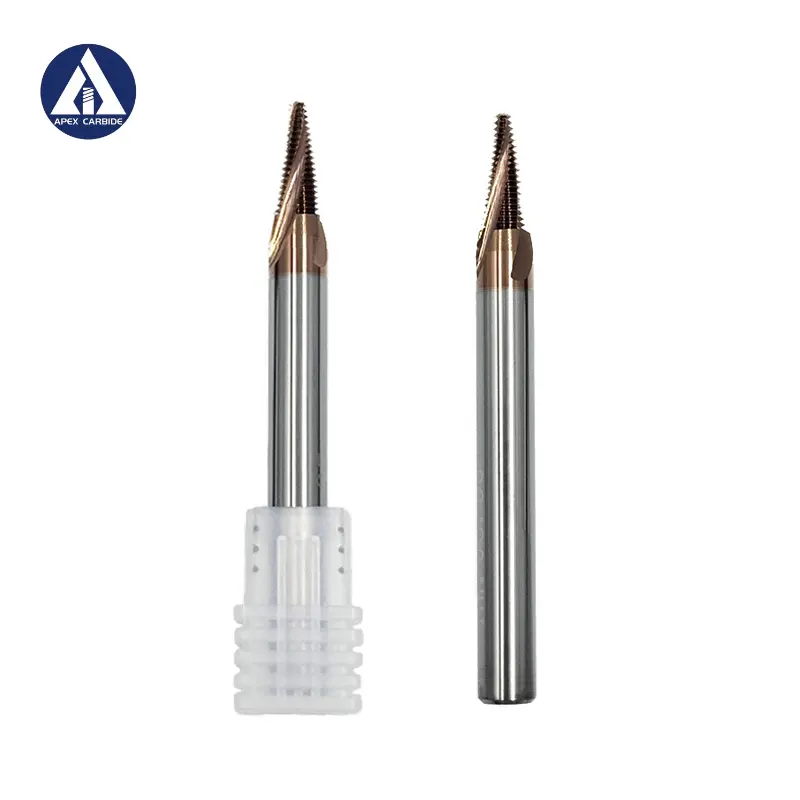
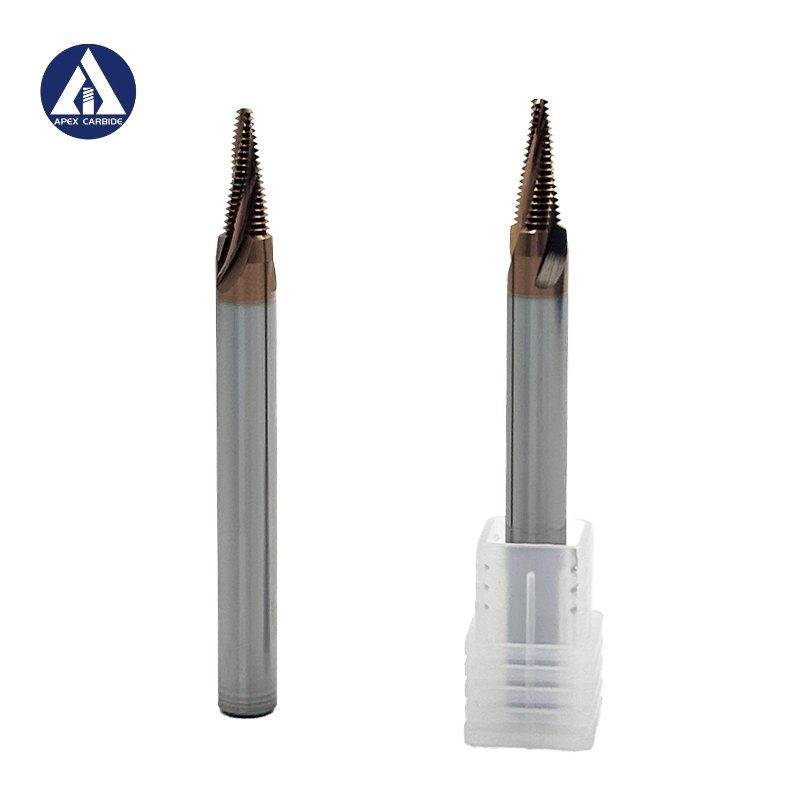
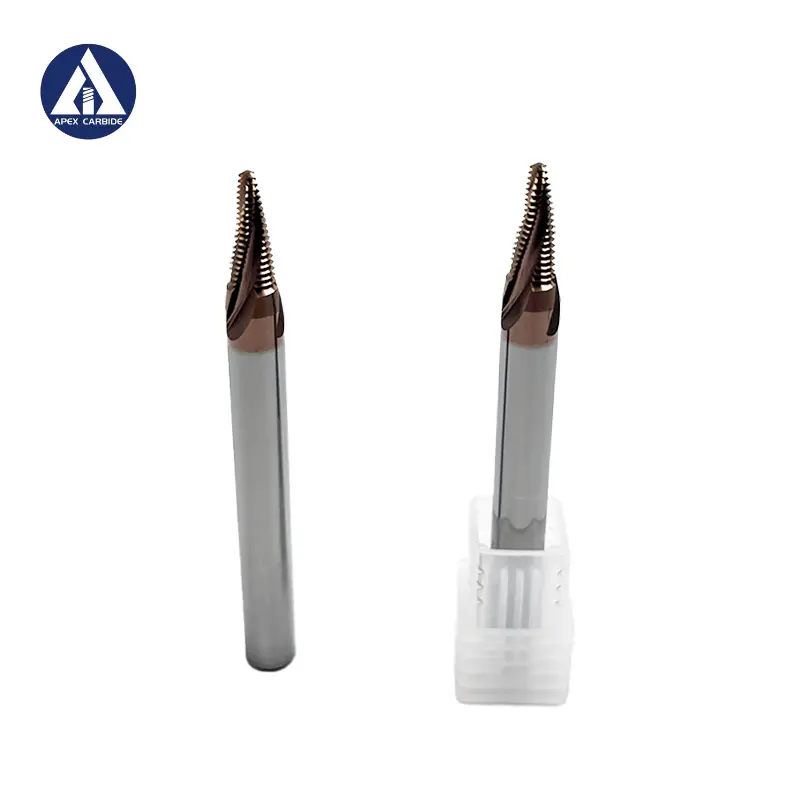
Wholesale Tapered Thread Milling Cutter with TiALN Coating Manufacturers, Factory
Product Description
Our Normal Sizes for ball nose tapered end mill
| Item code | Number of Flute |
R(mm) | A(") | d(mm) | F(mm) | L(mm) |
| cutting Radius |
Taper Radius |
shank Dia | flute length | overal length | ||
| APGM2BC-R0.25-15-H4 | 2 | 0.25 | 6.7° | 4 | 15.0 | 50 |
| APGM2BC-R0.5-15-H4 | 2 | 0.50 | 5.7° | 4 | 15.0 | 50 |
| APGM2BC-R0.75-15-H4 | 2 | 0.75 | 4.8° | 4 | 15.0 | 50 |
| APGM2BC-R1.0-15-H4 | 2 | 1.00 | 3.8° | 4 | 15.0 | 50 |
| APGM2BC-R0.25-20.5-H4 | 2 | 0.25 | 4.9° | 4 | 20.5 | 50 |
| APGM2BC-R0.5-20.5-H4 | 2 | 0.50 | 4.2° | 4 | 20.5 | 50 |
| APGM2BC-R0.75-20.5-H4 | 2 | 0.75 | 3.5° | 4 | 20.5 | 50 |
| APGM2BC-R1.0-20.5-H4 | 2 | 1.00 | 2.8° | 4 | 20.5 | 50 |
| APGM2BC-R0.25-20-H6 | 2 | 0.25 | 7.8° | 6 | 20.0 | 50 |
| APGM2BC-R0.5-20-H6 | 2 | 0.50 | 7.1° | 6 | 20.0 | 50 |
| APGM2BC-R0.75-20-H6 | 2 | 0.75 | 6.4° | 6 | 20.0 | 50 |
| APGM2BC-R1.0-20-H6 | 2 | 1.00 | 5.7 | 6 | 20.0 | 50 |
| APGM2BC-R1.5-20-H6 | 2 | 1.50 | 4.3° | 6 | 20.0 | 50 |
| APGM2BC-R2.0-20-H6 | 2 | 2.00 | 2.9° | 6 | 20.0 | 75 |
| APGM2BC-R0.25-30.5-H6 | 2 | 0.25 | 5.2° | 6 | 30.5 | 75 |
| APGM2BC-R0.5-30.5-H6 | 2 | 0.50 | 4.7° | 6 | 30.5 | 75 |
| APGM2BC-R0.75-30.5-H6 | 2 | 0.75 | 4.2° | 6 | 30.5 | 75 |
| APGM2BC-R1.0-30.5-H6 | 2 | 1.00 | 3.8° | 6 | 30.5 | 75 |
| APGM2BC-R1.5-30.5-H6 | 2 | 1.50 | 28° | 6 | 30.5 | 75 |
| APGM2BC-R2.0-30.5-H6 | 2 | 2.00 | 1.9° | 6 | 30.5 | 75 |
| APGM2BC-R0.5-47-H8 | 2 | 0.50 | 4.3° | 8 | 47.0 | 100 |
| APGM2BC-R0.75-47-H8 | 2 | 0.75 | 4° | 8 | 47.0 | 100 |
| APGM2BC-R1.0-47-H8 | 2 | 1.00 | 3.7° | 8 | 47.0 | 100 |
| APGM2BC-R1.5-47-H8 | 2 | 1.50 | 3° | 8 | 47.0 | 100 |
| APGM2BC-R2.0-47-H8 | 2 | 2.00 | 24° | 8 | 47.0 | 100 |
Other sizes could be made as per customers’requirement.
Tapered Thread Mill Product Overview
Core Machining Scenarios
Designed for dental implants, bone screws, and spinal systems. Precision machining of self-locking tapered internal threads for absolute sealing and micron-level positioning.
Fuel nozzles, hydraulic valves, and structural connectors requiring tight tolerances and high surface finishes.
Draft angle and threaded joint machining in deep cavities to optimize part ejection and cooling channel interfaces.
Tapered sealing surfaces for high-pressure valves and deep-sea drilling equipment, ensuring zero-leakage performance.
Tapered threaded holes in transmission housings, synchronizer cones, and engine blocks for high-torque structural strength.
Special Working Conditions
Optimized helical flutes and variable rake angles maintain stability on complex curved and slanted surfaces, suppressing chatter.
Tapered body provides superior rigidity over straight tools, reducing deflection and ensuring precise thread pitch at hole bottoms.
Handles materials above HRC55 with advanced heat-resistant coatings, performing well in dry or MQL conditions.
Optimized flute design ensures smooth chip evacuation when machining titanium, Inconel, and stainless steel, preventing chip wrapping.
Product Advantages
Wide range of angles to precisely match workpiece fit tolerances for a perfect self-locking result.
Cutting edges blend smoothly between thread and taper sections to reduce stress and prevent micro-chipping.
Ultra-fine grain imported carbide provides excellent hardness and toughness, even under interrupted cutting.
Produced on imported 5-axis CNC grinders with tool accuracy and taper repeatability within +/- 0.005 mm.
Standard AlTiN or TiAlN coatings block heat transfer, extending tool life by 40% to 80% on titanium and stainless steel.
Special edge treatment removes micro-burrs, improving internal thread finish and reducing secondary deburring costs.
Service & Supply Chain
From powder blending to finished tools, ensuring strict quality control and stable lead times.
Taper angles, flute lengths, overall lengths, flute counts, and coatings fully customizable. MOQ as low as 1 piece.
Standard items ship same/next day. Custom orders ship within 7 to 25 days after drawing approval. Monthly capacity of 1,000,000 pieces.
FAQ
A: Standard models for carbon, alloy, pre-hardened, and standard stainless steels. Reinforced models for hardened steel (HRC55+), titanium, and Inconel.
A: Taps break easily in deep or angled holes. Tapered thread mills offer stable cutting, smooth chip removal, and one tool can handle multiple taper sizes.
A: Yes, non-standard customization is our core strength. We rarely charge high development fees for standard adjustments; costs are based on actual machining difficulty.
A: If peeling or chipping occurs early and is verified as a manufacturing defect, we provide a free replacement.
A: Emulsion or MQL for steel; EP cutting oil for titanium and stainless steel, directed at the cutting edge for heat removal and chip flushing.
A: Samples in 7 to 10 working days. Mass production can begin and ship within one week after sample approval. Sample order accepted first.









