
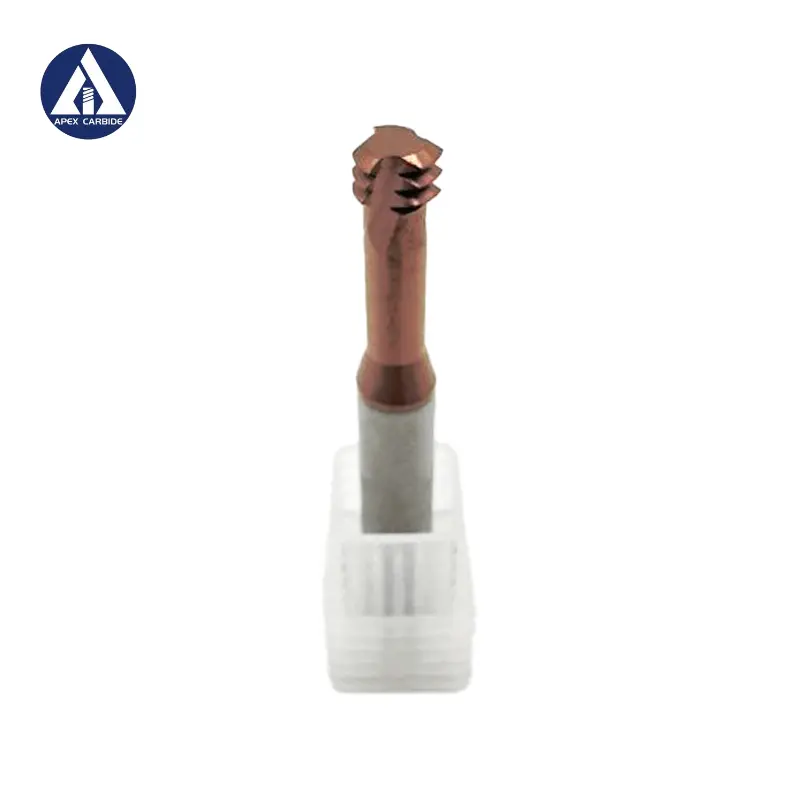
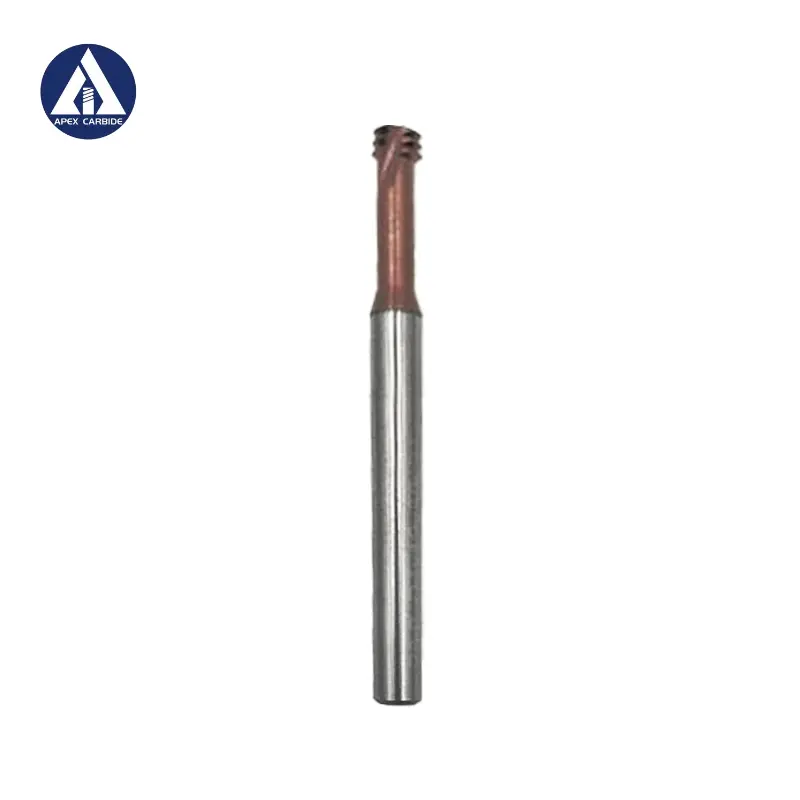
Wholesale Three tooth General machining thread end mill Manufacturers, Factories
Product Description
| Item Code | Thread Size | Pitch Size (mm) | Cutting Dia (mm) | Shank Dia (mm) | Working Length (mm) | Overall Length (mm) |
|---|---|---|---|---|---|---|
| APT-M1*0.25-H4 | M1 | 0.25 | 0.73 | 4 | 3 | 50 |
| APT-M1.2*0.25-H4 | M1.2 | 0.25 | 0.92 | 4 | 3.6 | 50 |
| APT-M1.4*0.3-H4 | M1.4 | 0.30 | 1.05 | 4 | 4.2 | 50 |
| APT-M1.6*0.35-H4 | M1.6 | 0.35 | 1.21 | 4 | 4.8 | 50 |
| APT-M2*0.4-H4 | M2 | 0.40 | 1.55 | 4 | 6 | 50 |
| APT-M2.5*0.45--H4 | M2.5 | 0.45 | 2.00 | 4 | 7.5 | 50 |
| APT-M3*0.5-H4 | M3 | 0.50 | 2.40 | 4 | 9 | 50 |
| APT-M4*0.7-H4 | M4 | 0.70 | 3.15 | 4 | 12 | 50 |
| APT-M5*0.8-H4 | M5 | 0.80 | 4.00 | 4 | 15 | 50 |
| APT-M6*1.0-H6 | M6 | 1.00 | 4.80 | 6 | 12 | 50 |
| APT-M8*1.25-H6 | M8 | 1.25 | 6.00 | 6 | 16 | 50 |
| APT-M10*1.5-H8 | M10 | 1.50 | 8.00 | 8 | 21 | 60 |
| APT-M12*1.75-H10 | M12 | 1.75 | 10.0 | 10 | 30 | 75 |
| APTN-M1*0.25-H4 | M1 | 0.25 | 0.73 | 4 | 3 | 50 |
| APTN-M1.2*0.25-H4 | M1.2 | 0.25 | 0.92 | 4 | 3.6 | 50 |
| APTN-M1.4*0.3-H4 | M1.4 | 0.30 | 1.05 | 4 | 4.2 | 50 |
| APTN-M1.6*0.35-H4 | M1.6 | 0.35 | 1.21 | 4 | 4.8 | 50 |
| APTN-M2*0.4-H4 | M2 | 0.40 | 1.55 | 4 | 6 | 50 |
| APTN-M2.5*0.45--H4 | M2.5 | 0.45 | 2.00 | 4 | 7.5 | 50 |
| APTN-M3*0.5-H4 | M3 | 0.50 | 2.40 | 4 | 9 | 50 |
| APTN-M4*0.7-H4 | M4 | 0.70 | 3.15 | 4 | 12 | 50 |
| APTN-M5'0.8-H4 | M5 | 0.80 | 4.00 | 4 | 15 | 50 |
| APTN-M6*1.0-H6 | M6 | 1.00 | 4.80 | 6 | 12 | 50 |
| APTN-M8*1.25-H6 | M8 | 1.25 | 6.00 | 6 | 16 | 50 |
| APTN-M10*1.5-H8 | M10 | 1.50 | 8.00 | 8 | 21 | 60 |
| APTN-M12*1.75-H10 | M12 | 1.75 | 10.00 | 10 | 30 | 75 |
General Steel Machining
Precision thread milling and general profiling of carbon steel, alloy steel, and medium-hard steel (HRC ≤ 45). Suitable for threaded holes, external threads, and thread profiling.
Mold & Die Components
Chamfering, thread bottoming, and precision finishing of mold bases, fixture parts, and mechanical hardware.
Automotive & Mechanical Parts
Thread machining of engine parts, gearbox components, hydraulic fittings, and standard fasteners.
3C & General Hardware
High-efficiency thread milling for aluminum housings, copper connectors, and general mechanical parts.
Hole Machining & Deburring
Three-tooth design ensures efficient hole edge finishing and thread preparation for assembly.
Dry Cutting Friendly
H-Si coating enables excellent high-speed dry cutting for general machining scenarios.
General Purpose Profiling
Balanced design for slotting, ramping, and light profiling operations in addition to thread milling.
Delivers 30%+ higher material removal rate for faster thread milling and boosted productivity.
Minimizes vibration, ensures precise thread profiles, and extends tool service life.
Excellent chemical stability, high hot hardness, and outstanding oxidation/wear resistance.
Ideal for high-speed dry cutting applications, reduces cutting heat and friction for better surface finish.
Made with top-grade APEX/Sandvik ultra-fine grain carbide for exceptional hardness and toughness.
Processed on Rollomatic/Walter/Anca machines for tight tolerances and strong coating adhesion.
20+ years of manufacturing expertise ensures stable supply and cost efficiency.
Custom diameters, lengths, thread specs available, with MOQ=1pc and fast lead times.









