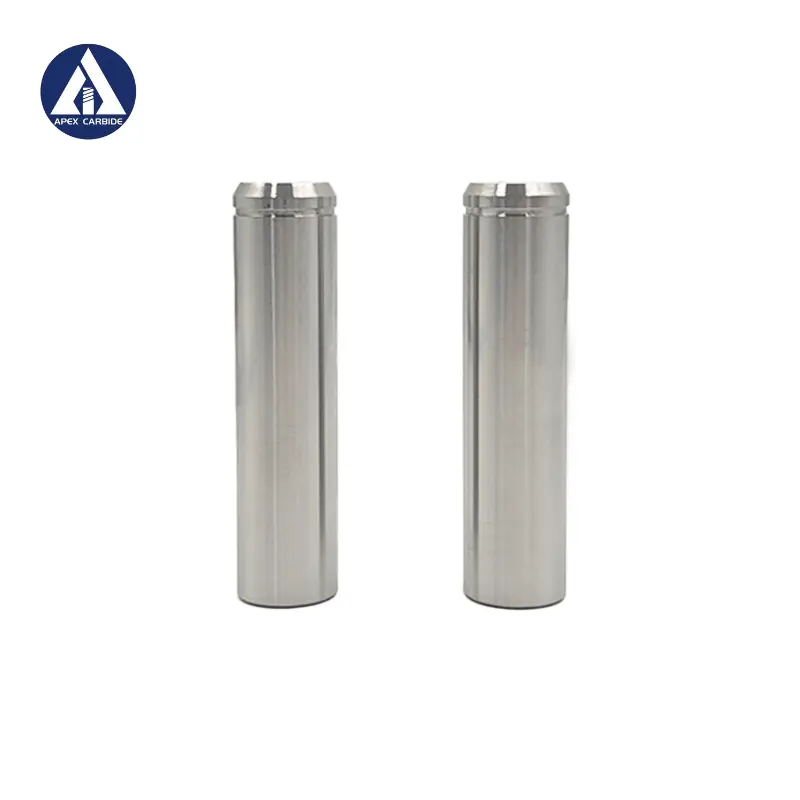
China Custom Tungsten Carbide Cylindrical Parts with Slotted Top Supplier, Suppliers
Product Description
Tungsten Carbide Rods Overview
Manufacturing Precision
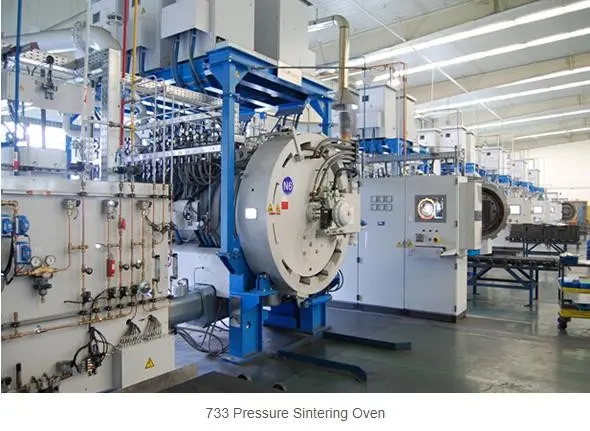
Formed through high-precision pressing or extrusion molding and processed through integrated low-pressure vacuum sintering furnaces for exceptional overall structural density.
Tolerances & Finishing
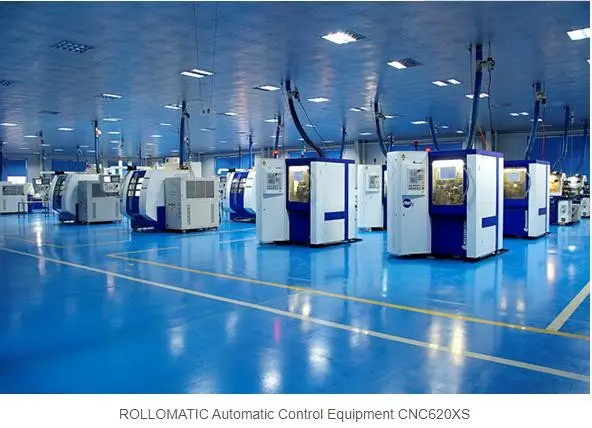
Available as rough blanks or precision-ground bars ground to tight tolerances (h5, h6, -0.005mm) with custom chamfering options tailored to production requirements.
Broad Machinability
Engineered for machining general steel, cast iron, stainless steel, heat-resistant steel, nickel-base alloys, and titanium alloys across standard and high-speed CNC operations.
Tooling Applications
Widely adopted as base material for cutting tools including solid carbide twist drills, end mills, reamers, taps, and high-precision gun drills.
Key Material Characteristics
- Superfine Raw Materials: Fabricated using premium superfine tungsten carbide powder for balanced toughness and hardness.
- 10MPa HIP-Sinter Technology: Sintered in standardized 10MPa overpressure vacuum furnaces to eliminate microscopic pores.
- High Mechanical Properties: Exceptional red hardness, wear resistance, elevated transverse rupture strength (TRS), and superior modulus of elasticity.
- Stable Physical Properties: Superior impact resistance, chemical stability, low thermal expansion coefficient, and iron-equivalent conductivity.
Tungsten Carbide Material Grade Specifications
| Grade | ISO Grade | Grain Size | Cobalt Content | Density | Hardness | TRS | Application Scope |
|---|---|---|---|---|---|---|---|
| μm | % | g/cm³ | HRA | N/mm² | |||
| A06 | K05-K10 | 1.0 | 6 | 14.95 | 92.60 | 4000 | Semi-finishing and finishing milling/drilling of materials (HRC 48-55) at medium-to-high speeds: stainless steel, heat-resistant alloys, die steel, cast iron, 7-series aluminum, and titanium alloys. |
| A06U | K05-K10 | 0.7 | 6 | 14.95 | 93.30 | 4000 | Mills and drills with D ≥ 0.8mm; widely used in woodworking industry tooling. |
| A06UF | K05-K10 | 0.4 | 6 | 14.90 | 93.80 | 4200 | Micro mills and drills with 0.4mm ≤ D ≤ 1.6mm. Superior centralized particle distribution offering outstanding stability and wear resistance. |
| A09N | K10-K20 | 0.2 | 9 | 14.40 | 93.60 | 4500 | Hardened steels below HRC60, non-alloy metals, high-hard plastics, composites, and titanium alloys. Nano-particle structure delivering ultra-high toughness for high-speed cutting tools. |
| A10F | K20-K30 | 0.7 | 10 | 14.45 | 91.80 | 4000 | Roughing and semi-finishing milling of heat-treated steel, common alloy steel, cast iron, and materials below HRC45. |
| A12U | K30-K40 | 0.4 | 12 | 14.25 | 92.30 | 4200 | Roughing and semi-finishing milling of metals (HRC 45-52), including stainless steel, aluminum alloys, alloy steel, and non-ferrous metals. |
| A12UF | K30-K40 | 0.4 | 12 | 14.14 | 92.80 | 4200 | High-grade formulation suitable for semi-finishing of high-hardness steels below HRC55. |
Types and Dimension Tolerances
| 1. Tolerance of Unground Long Rods | ||
|---|---|---|
| Size (D × L, mm) | Tolerance (mm) | |
| Diameter (D) | Length (L) | |
| D(1-3) × 310/330 | +0.30 ~ +0.55 | 0.00 ~ +4.00 |
| D(3-12) × 310/330 | +0.30 ~ +0.60 | 0.00 ~ +4.00 |
| D(12-20) × 310/330 | +0.30 ~ +0.65 | 0.00 ~ +4.00 |
| D(20-40) × 310/330 | +0.30 ~ +0.70 | 0.00 ~ +4.00 |
| 2. Tolerance of Unground Cut-to-Length Rods | ||
|---|---|---|
| Diameter Range (mm) | Tolerance of D & L (mm) | |
| L ≤ 70 mm | 70 < L ≤ 150 mm | |
| D < 5 | D(0.20~0.30), L(0.20~1.5) | D(0.25~0.35), L(0.20~1.5) |
| 5 ≤ D < 40 | D(0.25~0.35), L(0.20~1.5) | D(0.30~0.40), L(0.20~1.5) |
3. Ground Long Rods
Standard diameter tolerance is h5/h6 or customized according to drawing specifications. Standard length tolerance is 0.00 ~ +5.00mm.
4. Ground Cut-to-Length Rods
Standard diameter tolerance is h5/h6 (or custom requirement). Standard length tolerance is controlled within 0.00 ~ +2.00mm.
5. PCB Rods
Micro-grain carbide rods developed specifically for high-speed printed circuit board drilling and routing tools.
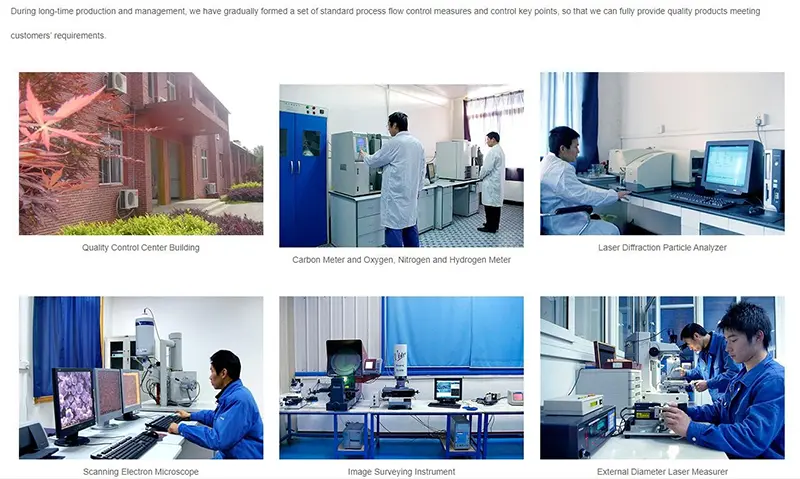
Manufacturing Capabilities & Quality Advantages